



Leather welding gloves look similar in a catalogue photo, but five variables drive both performance and cost: leather layer, lining, reinforcement, cuff length and stitching thread.
Split leather versus grain leather
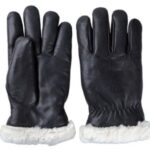
Cow split leather comes from the lower layer of the hide. It is thicker, more abrasion-resistant and more economical, which is why it dominates welding and heavy working gloves. Grain leather keeps the outer surface: softer, more flexible and more water-resistant, preferred for driver gloves where feel and comfort matter more than spatter resistance.
Lining and reinforcement
Full lining adds heat insulation and comfort for long welding sessions; unlined gloves are cooler and give better feel for short tasks. Reinforced palm, thumb and index finger extend life where the glove contacts hot workpieces and filler rod, and are usually the cheapest upgrade with the biggest effect on service life.
Length and pattern
Welding gloves commonly run from 11 to 24 inches. Longer cuffs protect the forearm from spatter when welding overhead. Working gloves are usually 10 to 16 inches. Clute cut and gunn cut patterns change flexibility and seam placement; gunn cut puts seams away from the palm contact area.
Что нам прислать
Tell us the welding process, typical amperage or heat exposure, whether operators need to feel small parts, and your target price. We will recommend split or grain, lining, reinforcement and length, and can supply matching aprons and sleeves from the same leather so body protection is consistent.